RED brings best-in-class, high-efficiency manufacturing technology from Europe and the U.S. to North American plants: SAT vertical finishing lines, GAT custom finishing systems, CitiUS industrial furnaces, ExtrusionSim press simulation, Rhopoint appearance and gloss meters, OptiSense coating-thickness systems, and coatingAI powder coating optimization.
Vertical powder coating, MAESTRO, anodizing and FOX.
Custom powder and paint lines: washers, ovens, conveyors.
Aging, homogenizing, annealing and casthouse lines.
Press recipes simulated before the die reaches the press.
RED Manufacturing Technologies brings North American plants the most efficient manufacturing technology in the world, engineered in Europe and the United States.
RED represents SAT vertical finishing lines, GAT custom finishing systems, CitiUS industrial furnaces, ExtrusionSim extrusion software, Rhopoint appearance and gloss meters, OptiSense coating-thickness systems, and coatingAI powder coating optimization across North America, with one point of contact from first conversation to running equipment.
Every line RED carries is a leader in its field, chosen because it outperforms what most North American plants run today.
Less floor space, less powder, less energy and fewer hands per part. Efficiency is the reason each technology is in the portfolio.
RED is run by people who have operated lines, not just sold them. We speak maintenance, changeovers and uptime.

Vertical lines do more in less space, with less handling and fewer chances to mark or bend long parts. For extruders and anyone finishing light poles, rack beams or other lineal products, the comparison that matters is output per square foot, color-change discipline, and what the line costs to run every day.
Published footprints of roughly 5,600, 6,630 and 8,290 ft², with outputs from about 300 to 1,000 profiles per hour depending on configuration.
SAT CUBE ↗Built for plants running varied order mixes and short lead times, where every changeover is lost capacity.
Profile recognition and recipe control take the guesswork out of gun settings. VISICOAT targets around 29% powder savings, and it runs with Gema dense-phase application.
Separate entrance and exit corridors and low-positioned fans for stable temperature, simpler maintenance and lower contamination risk.
SAT Trevisan ↗Less marring and bending, fewer hands on the part, and a line that keeps moving.
See it run ↗Complete SAT anodizing lines, plus FOX flash anodizing, a thin pretreatment layer under powder for demanding and marine environments.
SAT FOX ↗
MAESTRO is SAT's newest vertical powder coating line, built to get plants producing fast and to keep downtime short during the switch.
SAT joined Gema and the Graco group in 2018. North American customers get finishing-line expertise, Gema application technology and the stability of a U.S.-based parent.
Vertical powder coating lines, CUBE, MAESTRO, anodizing, FOX, VISICOAT, automated unloaders and related finishing equipment.
sataluminium.com ↗Automatic guns, powder centers, dense-phase handling, MagicControl and automation, with case studies on productivity and powder savings.
Gema extrusion finishing ↗American parent company with a broad industrial base, adding confidence around scale, support and long-term stability.
graco.com ↗
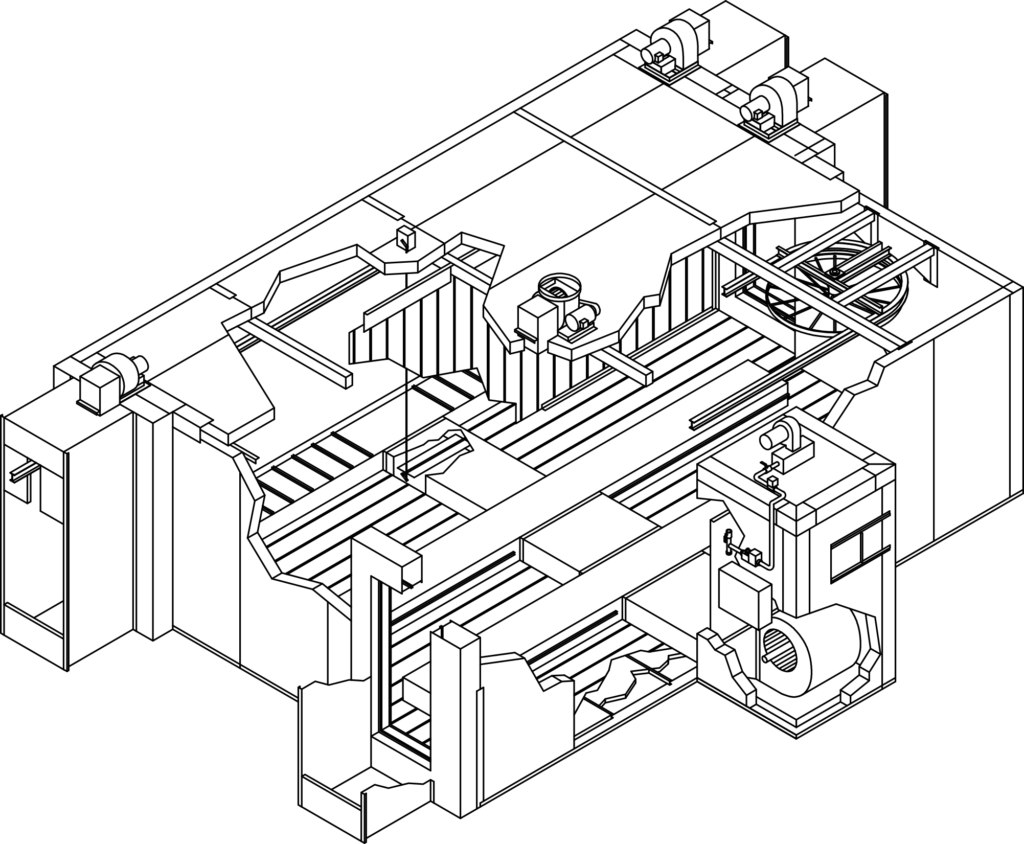
GAT Finishing Systems designs, builds and installs custom powder-coat and paint lines for manufacturers that want to stop losing margin, throughput and quality control to outsourcing or outdated equipment. The same team quotes the line, designs it, welds it, installs it and starts it up.

Multi-stage pretreatment in chemical-proof polypropylene housings, backed by a 10-year anti-corrosion warranty.
Direct-impingement convection ovens holding ±5 °F across the belt, and IR ovens that run 50–70% shorter than comparable convection ovens.
Overhead, power-and-free, mesh-belt and wicket conveyors under PLC control, plus climate-controlled powder coating rooms.

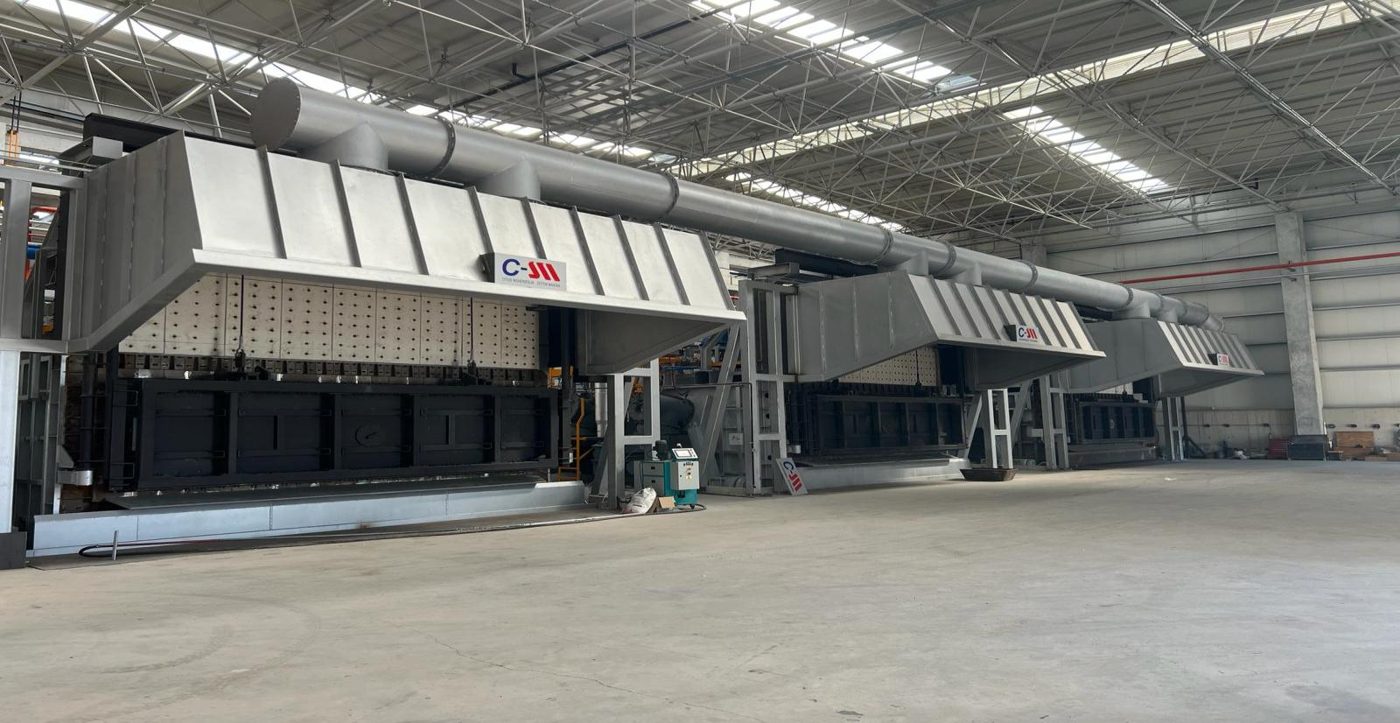
RED represents CitiUS of Istanbul in North America: industrial furnaces and complete thermal lines for aluminum and non-ferrous plants, engineered and built in Türkiye by a team led by founder Erdal Şahin, with 30 years in industrial furnaces.
Aging ovens for soft and hard alloys, billet heating, log homogenizing for extruders with their own melt shop, and high-bay basket storage.
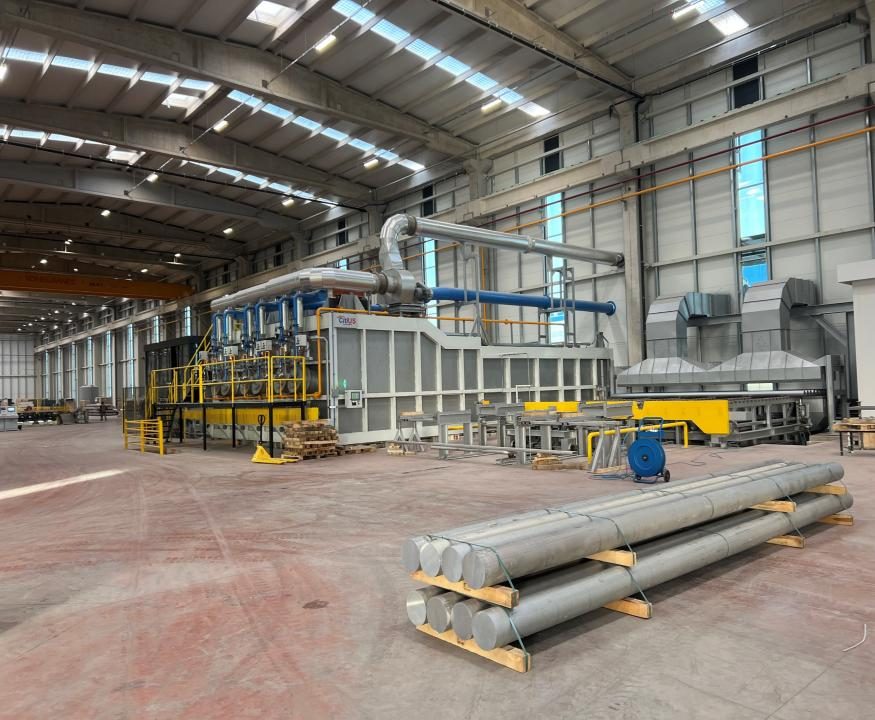
Melting and holding furnaces, homogenizing centres and complete log casthouse lines, from scrap charging to packing.
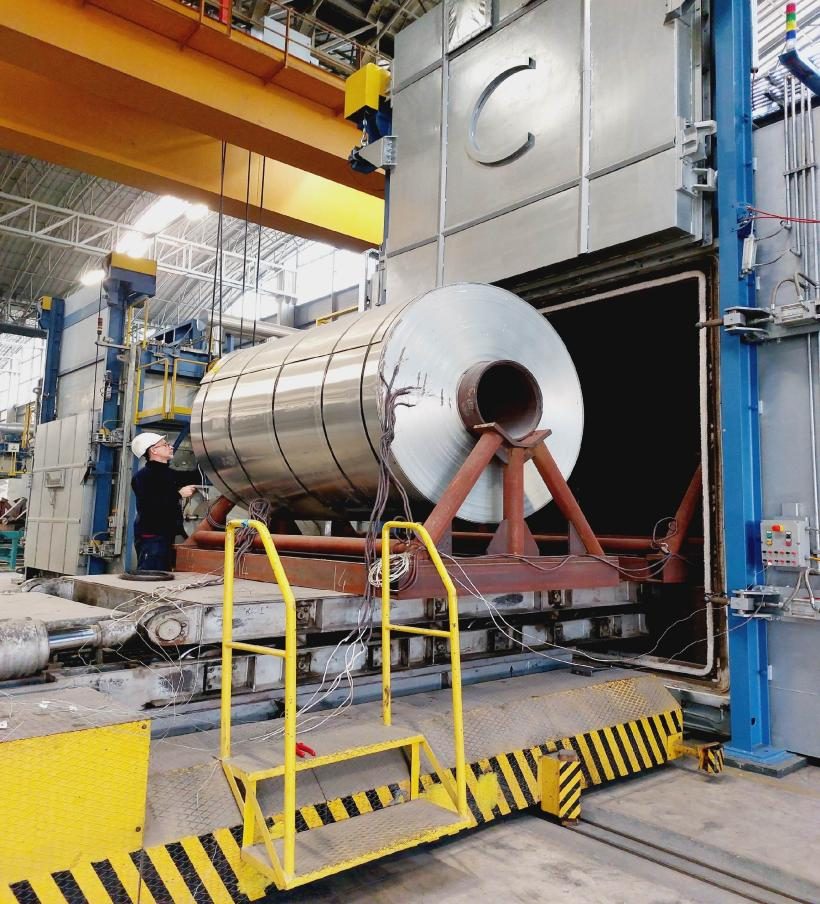
Coil and foil annealing, continuous slug annealing, tube and brass annealing, and solution heat-treatment lines.
Aging oven for an extrusion plant, 18 t per batch. In service since 2025.
Four electrically heated foil annealing furnaces, 40,000 lb per batch. In service since 2024.
Continuous slug annealing furnace, 2,500 kg per hour. In service since 2026.
ExtrusionSim (EIS3) simulates each extrusion job before it runs: billet, container and die temperatures, ram and puller speed, scrap, quench settings and cost per kilogram. The engine is built on nearly 30 years of production data from working extrusion plants and validated against real press output.
Nearly three decades of real-world extrusion data, cross-checked against measured output across alloys, die types and presses.
Isothermal extrusion in the Intermediate version; comprehensive thermal management in the Full version. Cloud or self-hosted.
Every calculation is available over a REST API, so ERP, Excel and in-house tools can drive simulations directly.
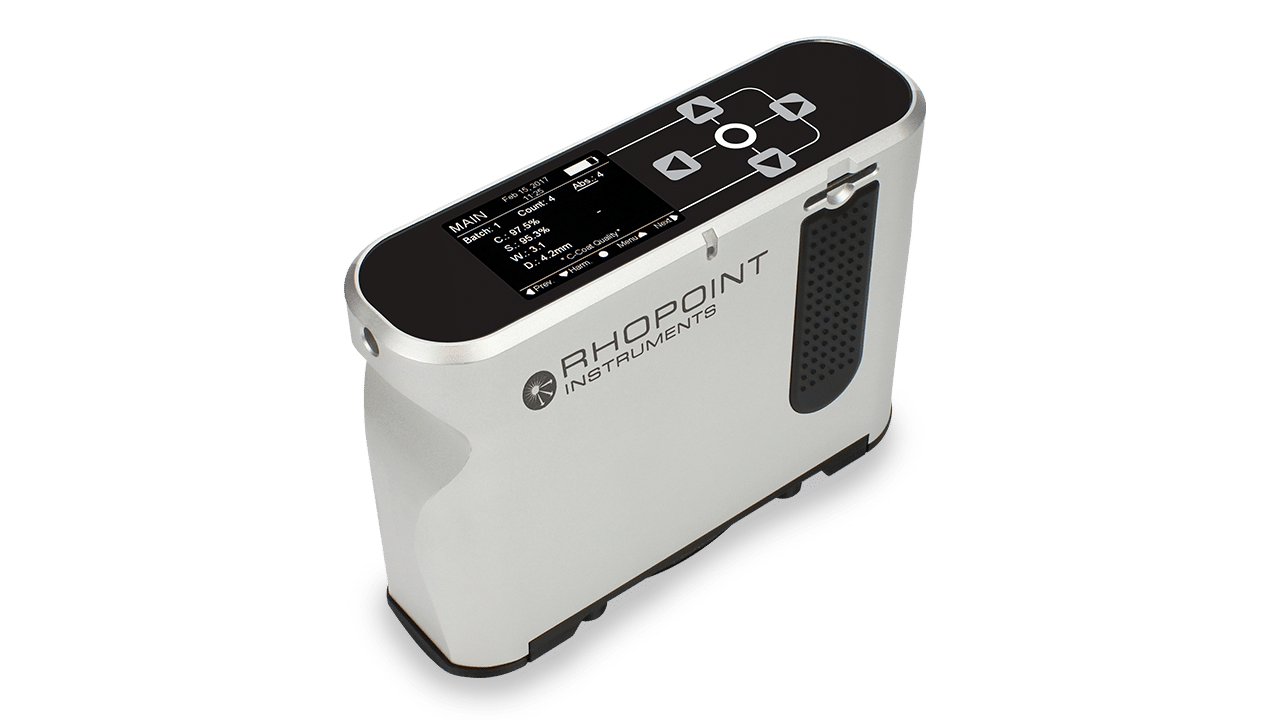
Documentation ↗RED represents Rhopoint Americas for powder coating and finishing customers across the USA and Canada. A glossmeter tells you how shiny a part is. Rhopoint now measures how it looks.

Rhopoint Aesthetix measures every aspect of how a surface looks: gloss, texture, topography, surface patterns and visual uniformity. It turns them into simple perception scores you can set pass/fail tolerances on.


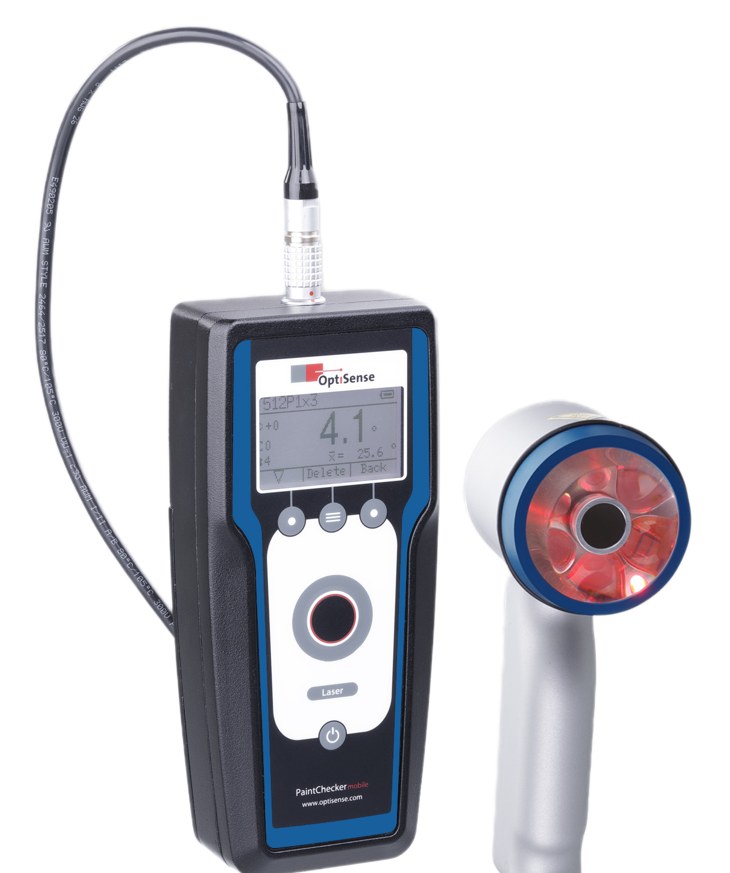
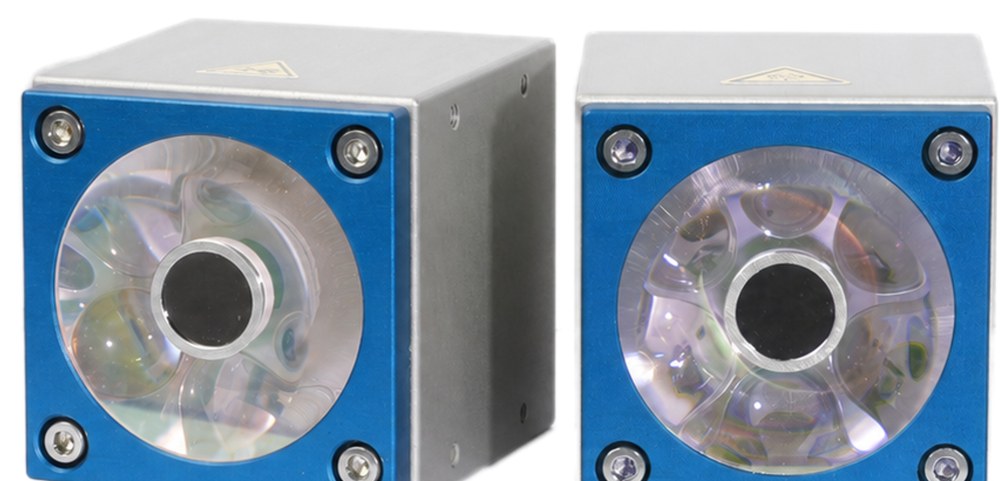
OptiSense PaintChecker non-contact coating-thickness systems, represented by RED through Rhopoint Americas across the USA and Canada. Measure film build before the oven, in the booth or on the line.

The Gun-B reads freshly applied powder before cure, on metal and other substrates, independent of color, and accounts for shrinkage during melting. Catch overcoating while you can still adjust, instead of reworking cured parts. Now available with 75 mm optics for more stand-off from soft, fresh or hot coatings.
Contactless and eye-safe. Separate lightweight sensor on a flexible cable, audible confirmation, USB export to Excel.
Request a demo ↗ OptiSense Mobile ↗
Fixed, fixture-mounted or robot-mounted thickness measurement right on the line. Up to 8 sensors per controller, PROFINET IO and serial interfaces, and real-time data that production and QA systems can use to adjust powder coating parameters. 75 mm optics, ±20° angle tolerance.
OptiSense Industrial ↗
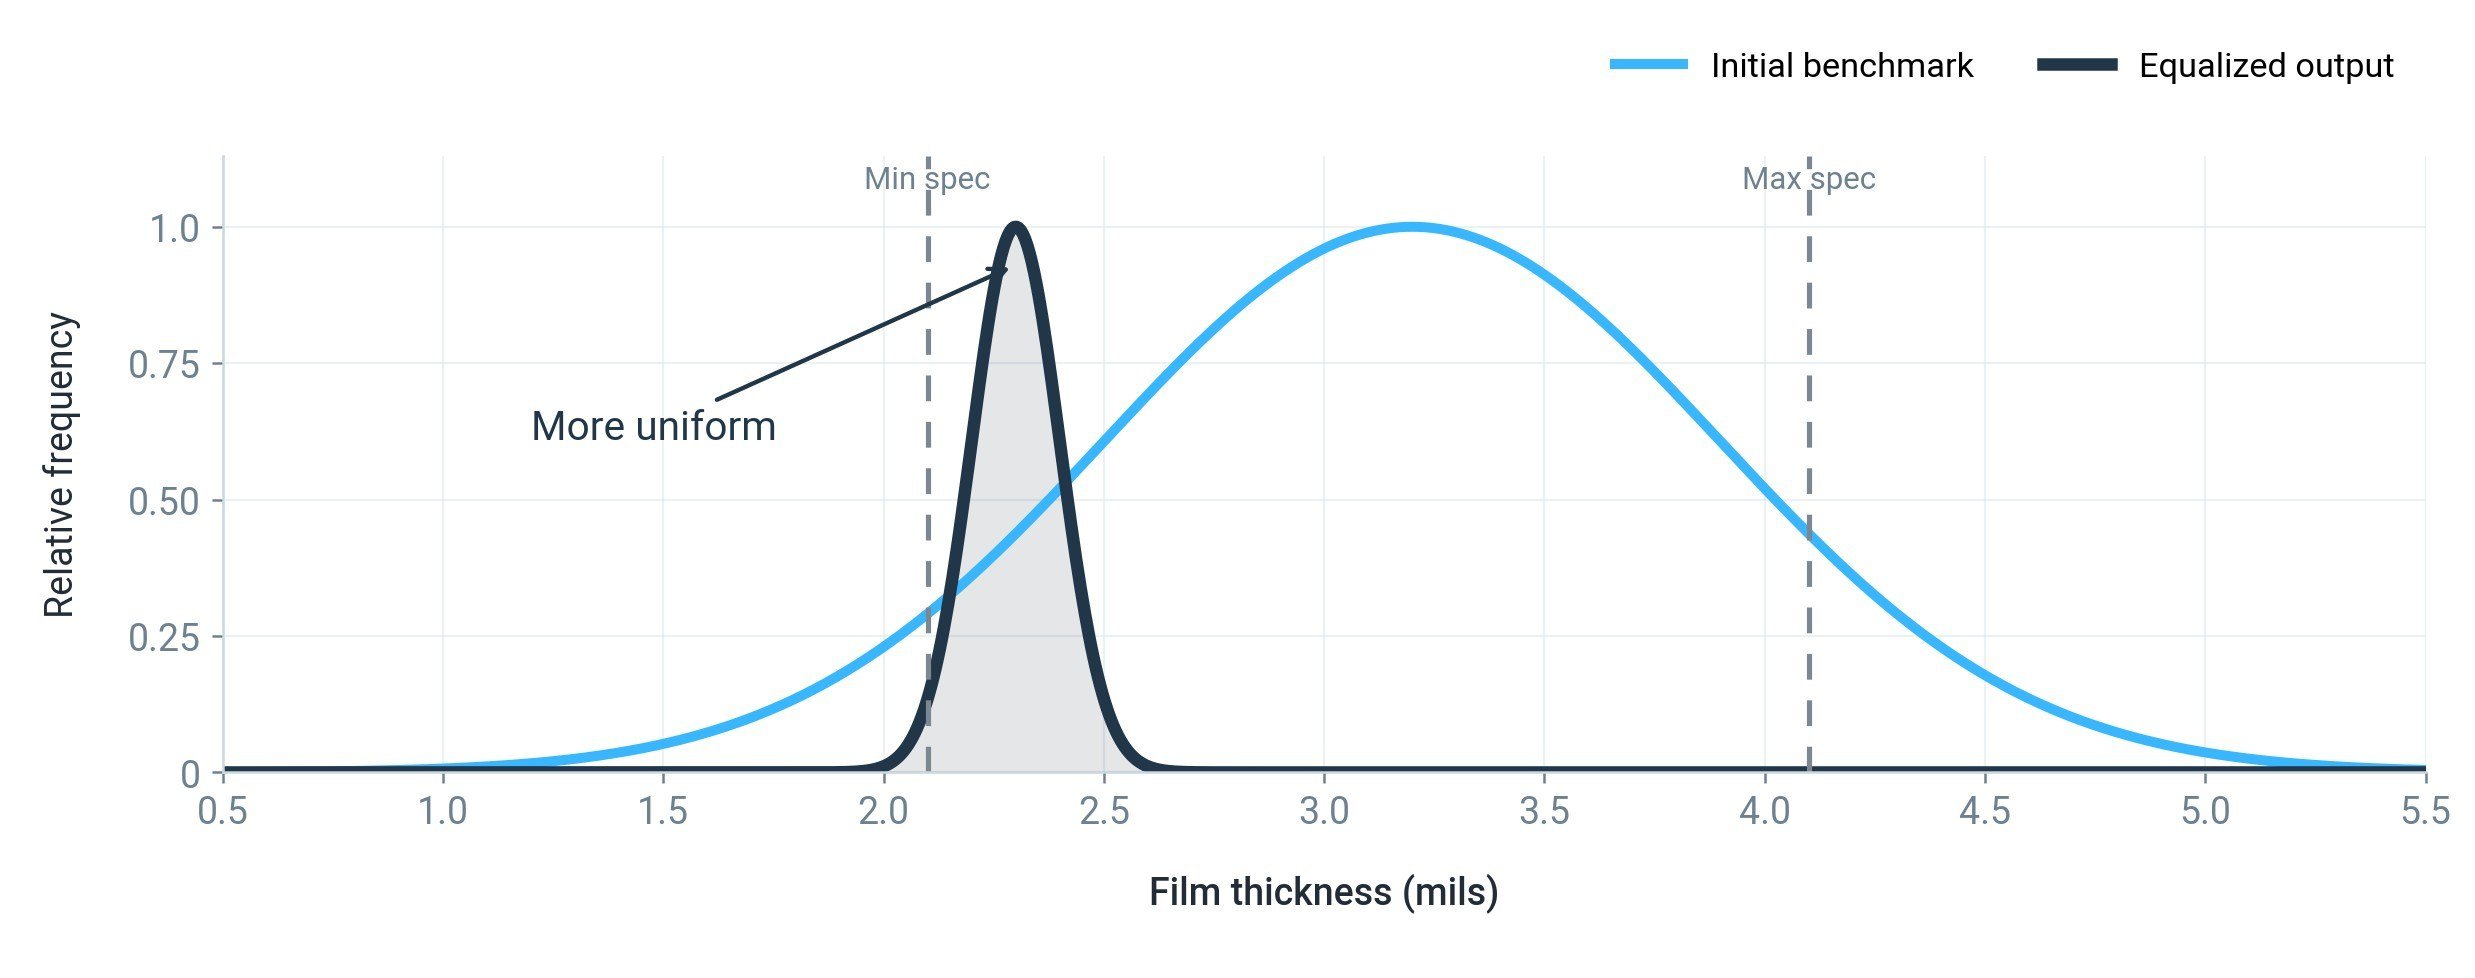
coatingAI's Blueprint OS uses AI to balance gun output and settings on your existing automatic powder line, so film build tightens around spec and less powder goes on the part. RED introduces North American coaters to coatingAI.
Example from coatingAI: equalizing powder output narrowed the film-thickness spread from 0.7 to 0.1 mils standard deviation, and the mean film build came down from 3.2 to 2.3 mils.
Current recipes, gun outputs and film thickness are measured on your line.
Guns and reciprocators are balanced during a short line-access window, typically at a shift change.
The change is measured while the required coating specification is held. 20 minutes a week keeps it there.
An onsite pilot measures the powder savings on your own line before you commit.
Set up while production keeps moving.
Higher first-pass yield and consistent settings from shift to shift.
Blaine has spent his career on the operating side of powder coating, as Finishing Supervisor at Madix and as Gema Territory Manager for Graco. He founded RED in 2026.
An accountant with an MBA, Gina leads RED's finance and contracts.
RED doesn't drop a brochure and disappear. We stay with the project until the line does what it is supposed to do.
Part mix, throughput target, building constraints, labor reality, and why the current process isn't good enough.
Color-change frequency, part geometry, pretreatment, automation goals, energy, and the cost of outside finishing.
Compare footprint, output, labor, powder use and process control against operating reality.
Coordinate the project with the manufacturer, commercially and technically, until you have a line you can run with confidence.
Finishing line, furnace, press software, measurement or powder savings: a 20-minute call is usually enough to know where RED can help.
Email sales@redmfgtech.com ↗